An industrial supermarket is a specialized inventory model designed to optimize the availability and flow of maintenance, repair, and operating supplies within complex production environments. Unlike a conventional retail store, this system functions as a structured, high-visibility warehouse that brings critical components directly to the point of use on the factory floor.

The core philosophy behind this approach is to bridge the gap between procurement logistics and operational efficiency, ensuring that operators and technicians have immediate access to the right parts at the right time. By applying standardized retail principles to the industrial sector, organizations can significantly reduce downtime, cut excess inventory, and improve overall asset reliability.

Core Operational Principles
The foundation of an effective industrial supermarket lies in its alignment with lean manufacturing philosophies, particularly the concept of just-in-time delivery. Instead of storing large quantities of items in distant warehouses, essential spares are consolidated in smaller, strategically located hubs near the machines they serve.

This model emphasizes visual management and standardized processes, allowing staff to quickly identify stock levels and reorder needs. The system relies on a structured relationship with suppliers to ensure that replenishment happens rapidly, often within hours, rather than waiting for traditional bulk delivery schedules.
Strategic Location and Layout

One of the defining features of this system is its physical placement on the shop floor. These supermarkets are typically located at the cell level or adjacent to key work centers, eliminating the need for personnel to travel long distances to retrieve tools or parts.
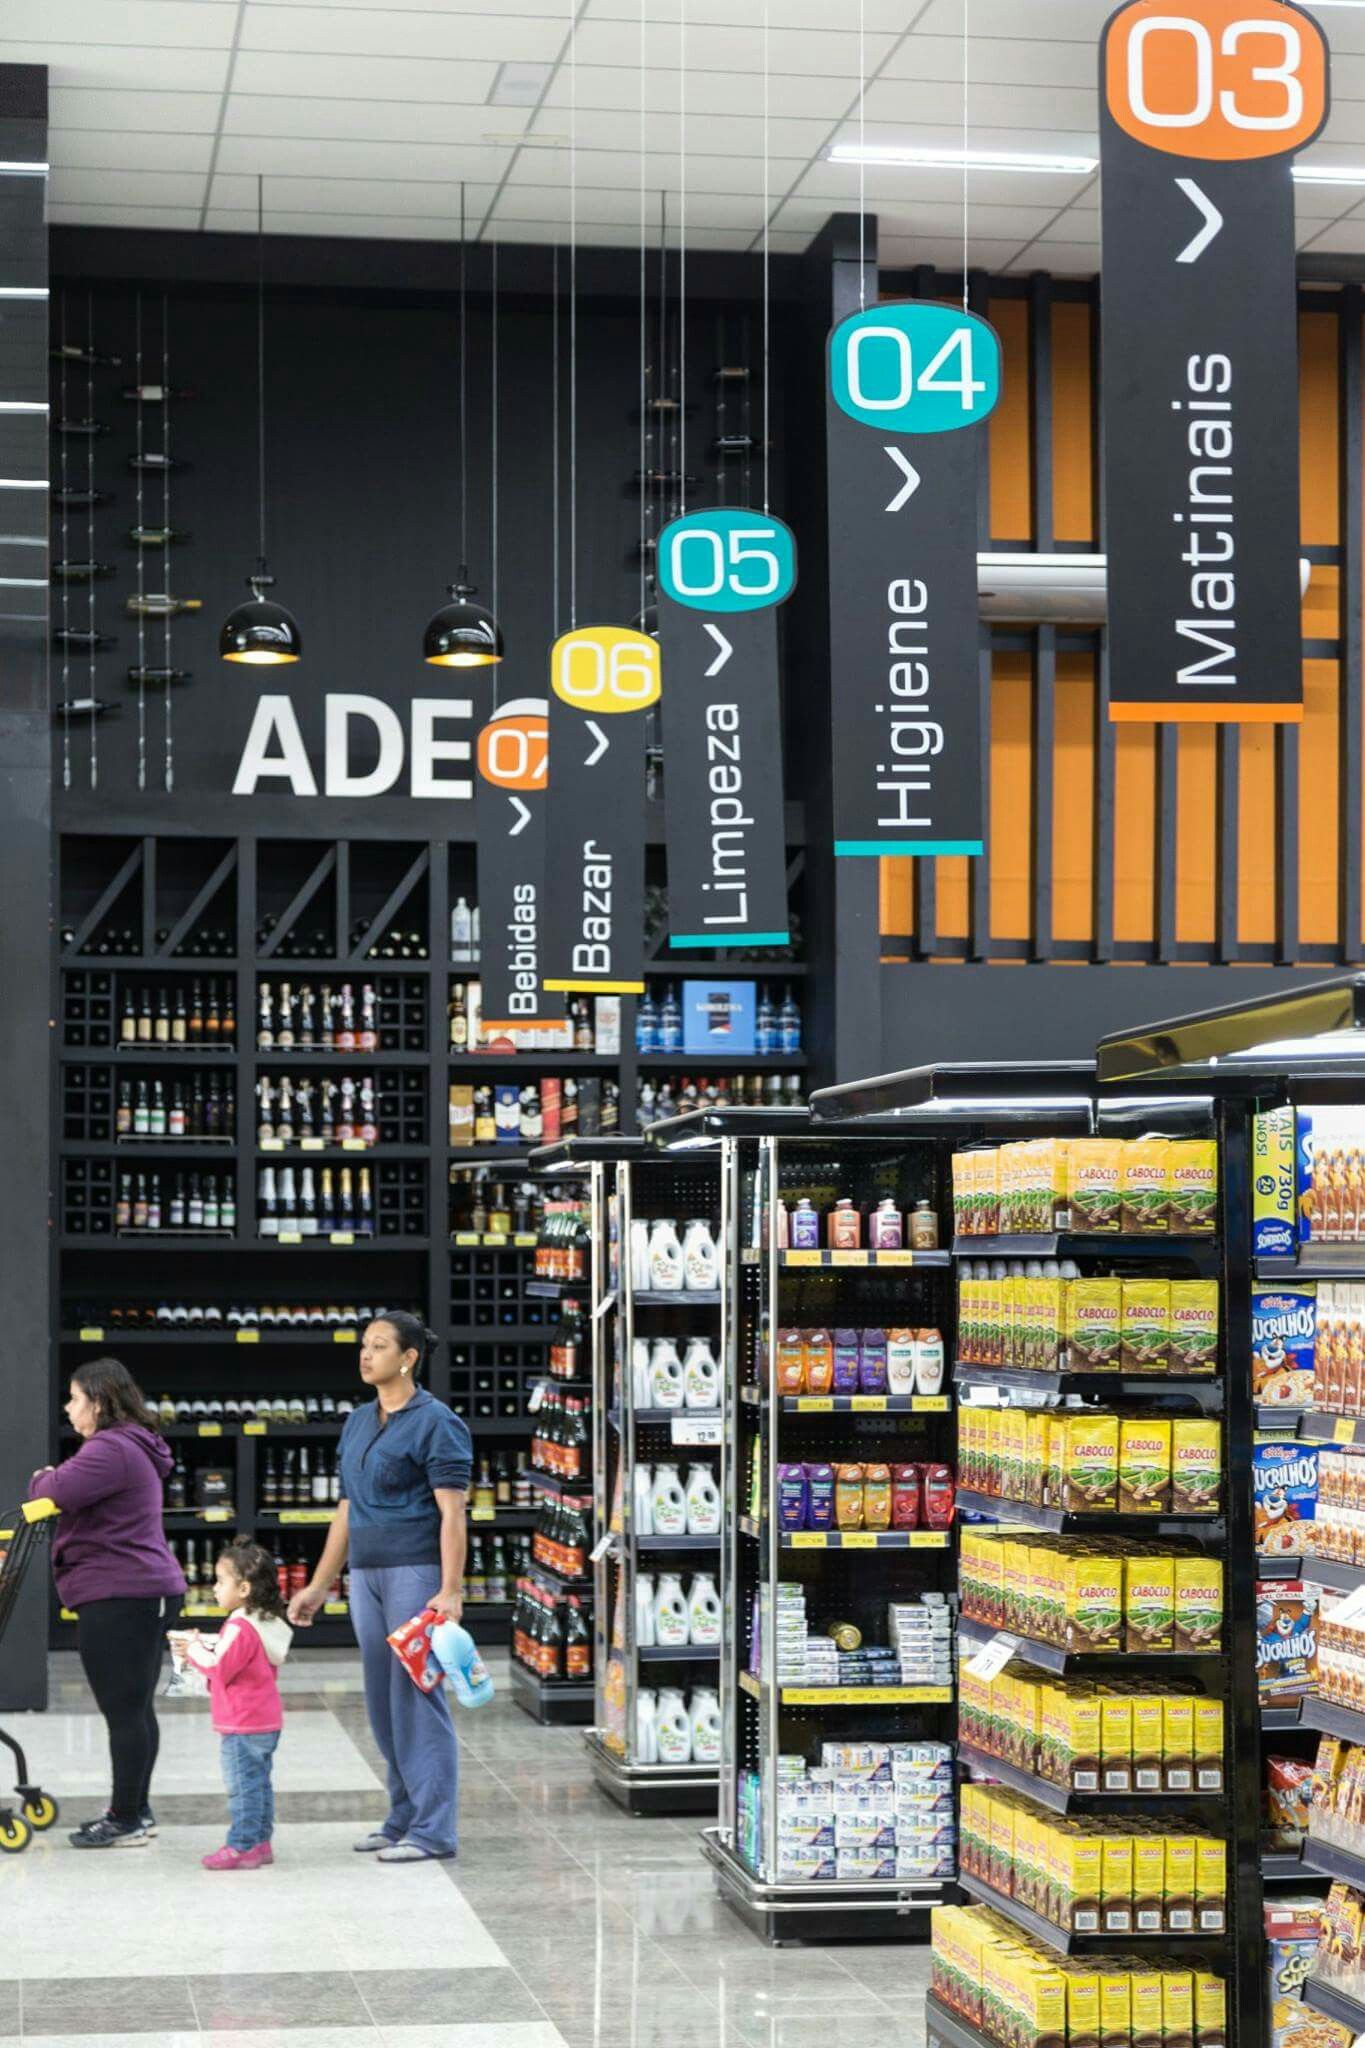
The layout is meticulously organized, often using color-coding and clear signage to guide users. Inventory is stored in standardized containers with visible maximum and minimum stock lines, ensuring that even in a high-noise, fast-paced environment, the workflow remains smooth and uninterrupted.
Inventory Management Techniques

Advanced inventory control is the backbone of this operation, utilizing both manual and digital tracking methods. Bins are tagged with unique identifiers and stock cards that record every withdrawal and delivery, providing a real-time audit trail.
Par levels are carefully calculated based on historical consumption data and equipment criticality, ensuring that high-value or frequently used items are always available while slow-moving stock is minimized. This precision prevents both production halts due to shortages and capital lockup due to overstocking.
Benefits and Impact on Efficiency

Implementing this model delivers a wide array of operational benefits that directly impact the bottom line. The most immediate advantage is the drastic reduction in machine downtime, as technicians no longer need to wait days for a missing gasket or bearing to arrive from a remote warehouse.
Furthermore, this system fosters a more organized and safer work environment. By consolidating tools and supplies into designated areas, it reduces clutter and trip hazards, contributing to a cleaner and more compliant facility that is easier to audit and manage.




Reduced Lead Times
Traditional procurement cycles can stretch over weeks, involving multiple approval layers and long-distance logistics. An industrial supermarket compresses this timeline to a matter of minutes or hours.
Technicians can walk to the supermarket, retrieve the part, and return to the task at hand immediately. This rapid turnaround translates to higher labor productivity and faster response times to emerging issues.
Cost Visibility and Control
By centralizing indirect spend on maintenance supplies, finance teams gain unprecedented visibility into consumption patterns. This transparency makes it easier to negotiate with suppliers and identify opportunities for substitution or standardization.
The reduction in obsolete stock and emergency airfreight costs further enhances profitability. The system essentially turns maintenance inventory from a hidden cost center into a measurable and controllable segment of the operational budget.
Enhanced Supplier Collaboration
Success in this model requires a shift in supplier relationships from transactional to collaborative. Vendors become partners responsible for maintaining virtual shelves on behalf of the buyer, ensuring that performance metrics regarding fill rates and delivery speed are met.
This partnership often leads to vendor-managed inventory (VMI) scenarios, where the supplier monitors stock levels remotely and proactively generates replenishment orders, further reducing the administrative burden on the client's team.
Standardization and Safety
The system promotes the use of standardized parts and components across equipment fleets, simplifying maintenance procedures and reducing the number of unique SKUs required. This consolidation makes training new staff easier and speeds up the troubleshooting process.
From a safety perspective, having a controlled environment for storing hazardous materials—such as oils, batteries, or chemicals—is a critical advantage. The supermarket acts as a secure point that complies with safety regulations, limiting the dispersion of dangerous goods across the site.
Embracing this structured approach to spare parts management represents a move toward smarter, data-driven operations that prioritize reliability and flow. By treating critical components with the same rigor as finished goods, organizations build a resilient foundation for continuous production and long-term competitive advantage.