In the demanding world of food production and preparation, safety and hygiene are non-negotiable. That's where food grade 304 stainless steel steps in – a material engineered to meet the strictest standards for food contact. But what exactly makes it 'food grade'? Let's unravel the science and specifications behind this industry staple.

What is Food Grade 304 Stainless Steel?
Food grade 304 stainless steel is a specific variant of the popular austenitic stainless steel grade 304, modified and certified to meet the stringent requirements for direct food contact.
While standard 304 stainless steel (also known as 18/8 stainless steel) is widely used, the 'food grade' designation ensures it adheres to regulations set by bodies like the FDA (U.S. Food and Drug Administration) and the EU's EC 1935/2004.
This grade maintains the same core composition (18% chromium, 8% nickel) but undergoes additional processing to eliminate contaminants and achieve a smoother surface finish, reducing the risk of bacterial growth.
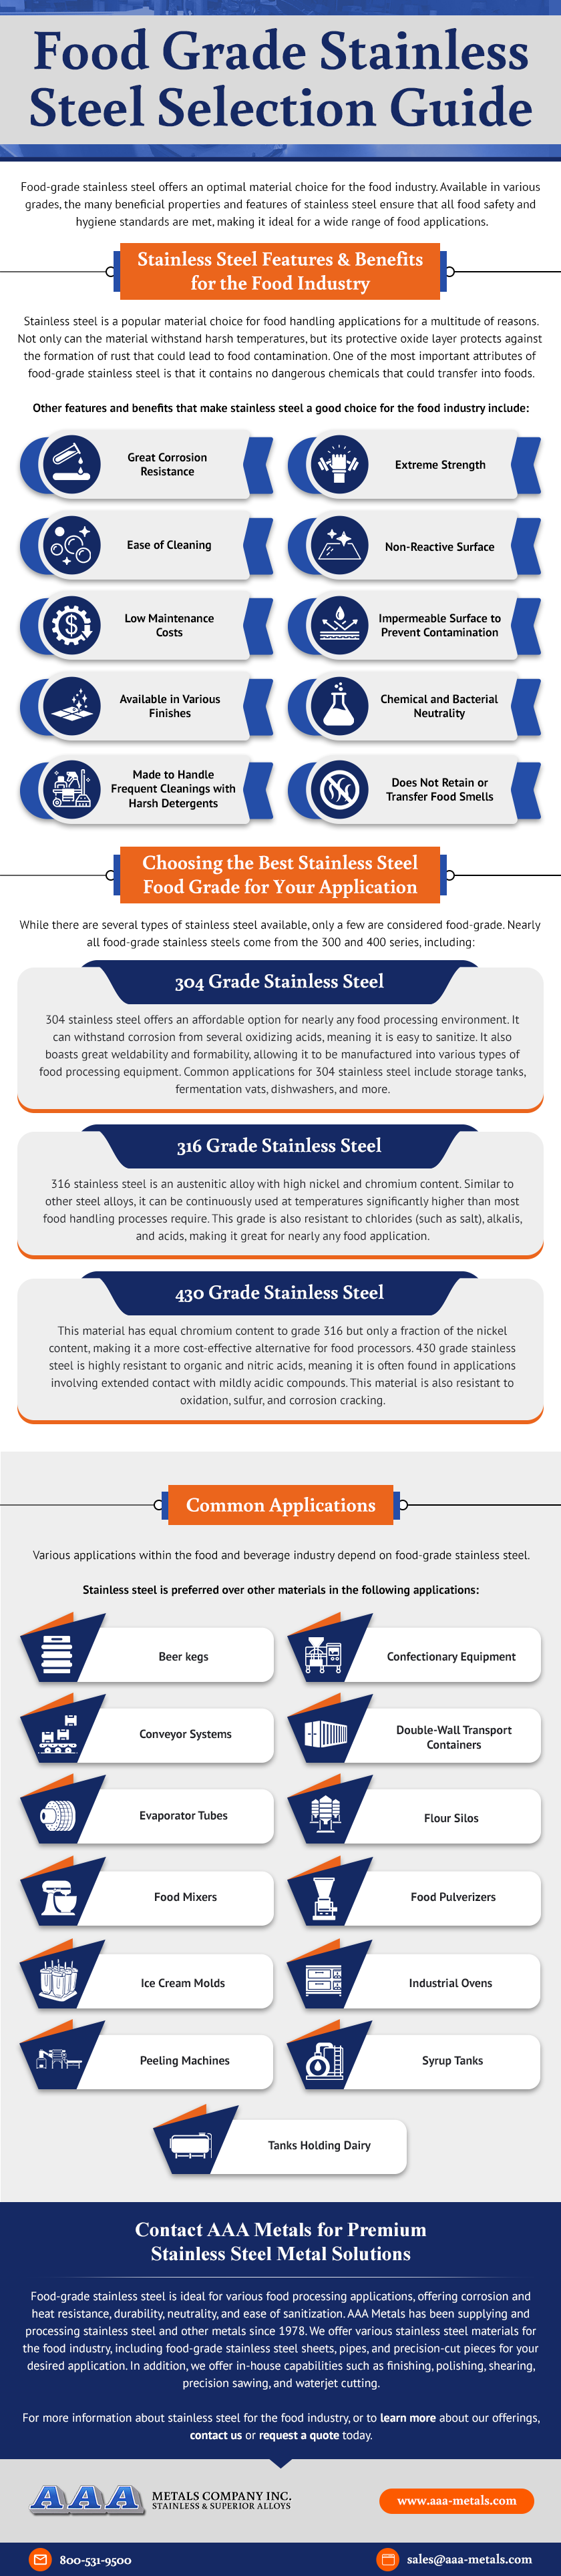
Key features include exceptional corrosion resistance, durability, and ease of cleaning – making it the go-to material for equipment that comes into contact with food and beverages.

Why is Food Grade 304 Critical for Food Safety?
The food industry operates under rigorous safety protocols. Food grade 304 stainless steel is pivotal because it prevents contamination and ensures product integrity.
Unlike lower grades or non-stainless materials, 304 food grade resists rust, staining, and chemical reactions with acids, salts, and other food components.
Its non-porous surface is virtually impervious to bacteria, mold, and other pathogens, which is critical for maintaining hygiene in environments like commercial kitchens, food processing plants, and beverage production facilities.
Moreover, it doesn't impart any flavors or odors to food, preserving taste and quality.
Compliance with global food safety standards means manufacturers can trust that their equipment won't compromise product safety or lead to regulatory violations.
Common Applications and Advantages of Food Grade 304
From the kitchen of a Michelin-starred restaurant to the assembly line of a global food manufacturer, food grade 304 stainless steel is ubiquitous.
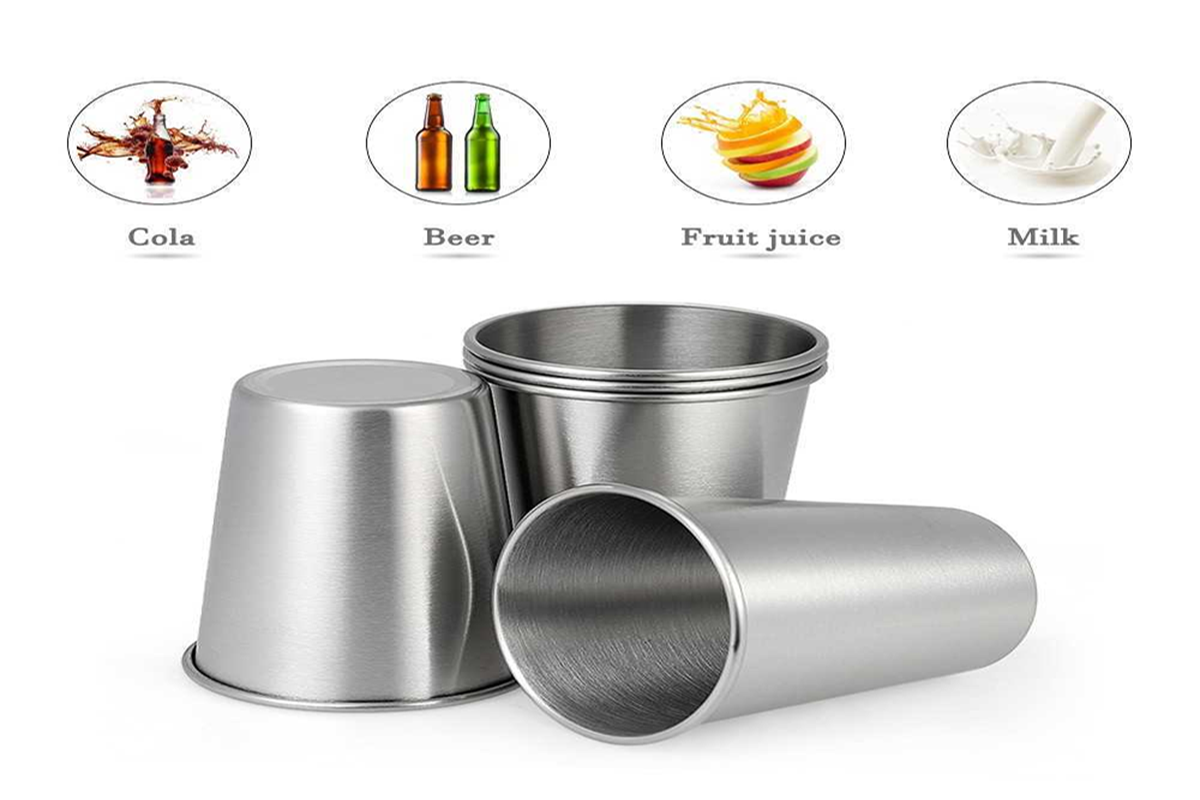
It's the material of choice for items such as mixing bowls, storage tanks, piping systems, conveyor belts, and even culinary tools like knives and spoons.
Its versatility extends to dairy processing, baking, beverage production, and pharmaceuticals.
Beyond safety, it offers unmatched durability and longevity, reducing replacement costs.
The material is also recyclable, aligning with sustainability goals.
When investing in food processing equipment, specifying food grade 304 ensures compliance, safety, and operational efficiency – a smart choice for any business committed to quality.
Understanding what food grade 304 stainless steel is and its critical role in food safety is essential for anyone in the food industry. Whether you're a manufacturer, chef, or quality control specialist, choosing the right materials isn't just about compliance – it's about protecting consumers and building trust. Ready to upgrade your equipment? Consult with a reputable supplier to ensure your food contact surfaces meet the highest standards.